The Quick-Choice Moment: Why Shape, Grip, and Flow Matter More Than You Think
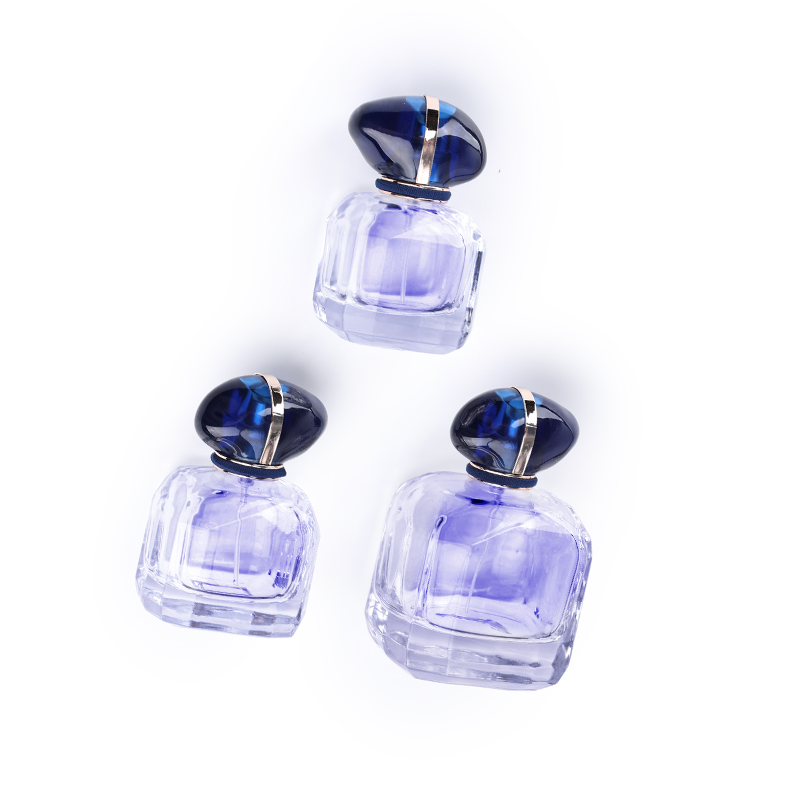
You step into a store, running late, and still need a gift. The round perfume bottle sits easy in your palm as you scan the shelf. Retail studies say many fragrance decisions happen in under ten seconds, and that short window is not just about looks—it is about comfort, control, and trust (even if you do not say it aloud). Speak to a seasoned round perfume bottle manufacturer, and they will confirm that hand feel, centre of mass, and pump feel are silent deal-makers. The glass radius guides how the thumb meets the sprayer actuator; the base weight steadies the aim; the neck finish decides if the pump sits flush. Now ask yourself: when speed is high and attention is split, what quietly steers your choice—shine, or control? The answer sits at the junction of ergonomics and process. We will go deeper into what breaks down in the real world, and how to see it before it costs you. Let us move from the shelf to the line.
The Hidden Frictions When You Source Round Bottles
What are we missing, really?
Here is the hard truth: most sourcing pain shows up after your first run, not during sampling. And it starts at the neck. If the neck finish drifts, even by fractions, closure torque swings. Pumps then leak, or mist poorly. A great round bottle can fail because the sprayer actuator does not seat square. Look, it’s simpler than you think: tolerance stacks ripple. Glass cools unevenly if the annealing lehr profile is off. Then caps wobble, collars tilt, labels creep on curves. The result? A beautiful pack that does not perform on busy lines. That gap between “sample pretty” and “line ready” is where money disappears—quietly.
Traditional fixes often miss the cause. Visual checks pass, but functional tests lag. Teams judge flint glass by clarity and forget base balance. They approve frosting tone, but ignore how coating adds microns that alter fit. Screen printing looks sharp on flat proofs; on curved glass, small stretch lines show later. And minimum orders force you to accept mixed cavities across ISO moulds, which means subtle shape variance. Those small shifts mess with pump crimp, cap click, and carton fit—one change snowballs into three. The better path is to design for assembly first, then for shine. That order saves runs, not just regrets.
From Guesswork to Measured Design: New Principles That Change the Game
What’s Next
The next wave is measurement-led. Not hype—methods. Good round perfume bottle manufacturers are mapping curvature, neck rings, and thread pitch with 3D scanning. They run SPC on inner bore diameters and hold a verified torque window for caps. Inline vision rejects warpage early, before cartons seal. Weight is tuned to balance grip without overspending glass. Coatings move to plasma or UV-curable films that add slip resistance yet keep clarity. Even colour drift shrinks when batch recipes lock to spectro targets. And recycled cullet ratios rise, while form stays consistent—funny how that works, right?
Compare this with the old approach: pick by look, then chase issues on the filler. The new path builds for function first. A pump spec aligns with neck tolerance; crimp or screw fit verifies under heat and cold cycle; print sits with controlled wrap on radius. You get a clean atomisation, a smooth actuator feel, and fewer line stops. The glass still shines, but performance leads. Over time, data closes the loop—drop tests inform base thickening, and alignment pins guide cap seating. The win is not only fewer rejects; it is a calmer, faster launch (and happier teams on the line).
How to Choose Smart: A Quick Checklist You Can Use Today
We have seen why the round form sells fast, and why unseen errors cost more than a fancy finish. To choose better, use three clear metrics—track them, not just talk about them.
1) Dimensional capability of the neck finish: demand evidence of tolerance control with Cpk or equivalent, plus gauges for inner bore and thread profile. If the fit is right, pumps behave right. 2) Sealing and spray performance under stress: test leak rate and atomisation after thermal cycling and vibration, at defined closure torque. No guesswork, only numbers. 3) Surface and print durability on curves: run adhesion and rub tests after coating or frosting, with wrap alignment checks on the exact bottle radius. If these three hold, most late surprises vanish.
Keep it steady, keep it simple, and let function lead form. In the end, round bottles are about hand, eye, and flow working as one. That is the calm centre of a good pack. NAVI Packaging